


loc
Visit us in our warehouse in Oakville, ON, or call us today to find out how MB Food Equipment can help serve your needs.
Feel free to browse our used food equipment inventory.
Our Products
In our showroom you will find only quality products from famous brands.
Newest Added Items
Check some of the newest products in our inventory
Contact Us
If you have any questions about our inventory or product details please give us a call or fill out the contact form and one of our sale managers will contact you.
Phone: (289) 993-5999
Phone: (289) 938-9348
Monday: 9 am – 5 pm
Tuesday: 9 am – 5 pm
Wednesday: 9 am – 5 pm
Thursday: 9 am – 5 pm
Friday: 9 am – 5 pm
Saturday: 9 am – 5 pm
Sunday: closed, by appointment only
After hours – by appointment
Contact form
Used Packaging Equipment Richmond Hill
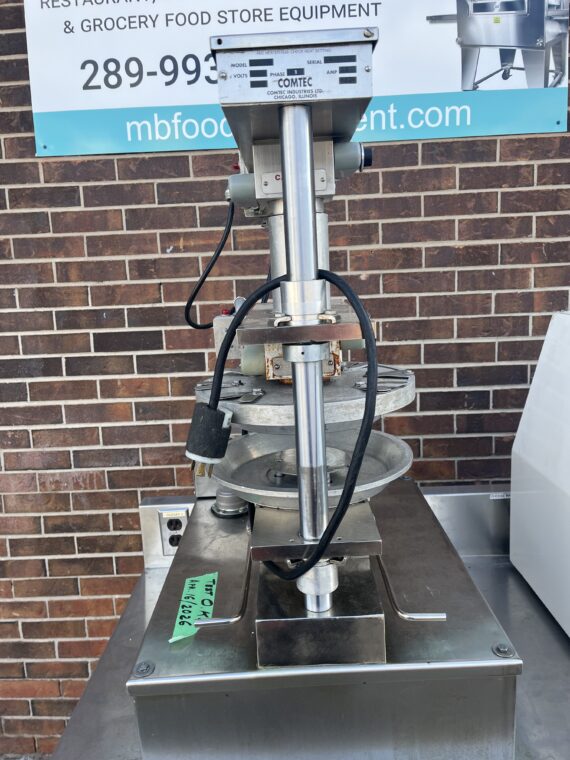
Used packaging equipment in Richmond Hill serves food businesses across the city looking to control capital expenditure without sacrificing functionality. MB Food Equipment specializes in sourcing, evaluating, and delivering reliable secondhand packaging machinery to bakeries, delis, grocery operations, and food manufacturers throughout the Greater Toronto Area, including Richmond Hill's growing food service sector.
1. Thermal and Mechanical Specifications Matter More Than Age
When evaluating used packaging equipment, the operational specifications-not the manufacture date-determine whether a machine will perform reliably in your operation. MB Food Equipment inspects critical components: heating element output (measured in watts or BTUs), seal strength consistency (typically 2.5 to 4.5 inches depending on application), and motor horsepower ratings. A ten-year-old vacuum sealer with verified heating performance and functional thermal controls often outperforms a newer unit with unverified component condition.
Richmond Hill businesses benefit from this specification-first approach because equipment sourced through MB Food Equipment is tested against operational baselines before delivery. Seal width, cycle time (how quickly a machine completes one packaging cycle, typically 3 to 8 seconds for commercial units), and consistency across repeated operations are documented, not assumed.
2. Seal Quality and Film Compatibility Drive Long-Term Cost
The total cost of ownership for packaging machinery extends far beyond the purchase price. Seal integrity-how completely and durably the machine bonds film layers-directly impacts product shelf life, waste rates, and customer satisfaction. Used equipment performing at 85 to 95 percent of original seal specifications will generate consistent output, whereas machines below 80 percent efficiency create costly waste and product loss.
Equipment sourced by MB Food Equipment for Richmond Hill customers is matched to your intended film types and thickness. Whether you require low-density polyethylene (LDPE), high-density polyethylene (HDPE), or specialized barrier films, the machinery must accommodate your material specifications. Incompatibility results in failed seals, spillage, and downtime-expenses that quickly exceed the savings from purchasing used equipment at discount rates.
3. Preventive Maintenance Records Reduce Downtime Risk
Commercial packaging equipment operates continuously in food service environments, making maintenance history a reliable predictor of future reliability. When MB Food Equipment evaluates equipment from other businesses, documentation of regular calibration, seal bar replacement, and motor servicing is examined carefully. Equipment with maintained service logs typically requires minimal adjustment after delivery, while units with incomplete history may need component replacement within the first weeks of operation.
For Richmond Hill food businesses, downtime during peak production periods is expensive. A packaging line that halts unexpectedly can delay order fulfillment, strain staffing, and damage customer relationships. MB Food Equipment prioritizes equipment with verifiable maintenance history because that history correlates directly with operational reliability in your facility.
4. Space Constraints Require Precise Footprint Measurement
Used packaging equipment varies significantly in physical footprint, even among machines with similar output capacity. A horizontal form-fill-seal (HFFS) machine may occupy 8 feet by 4 feet of floor space, while a comparable vertical form-fill-seal (VFFS) unit requires only 5 feet by 3 feet. Richmond Hill facilities with space limitations-common in compact urban locations and existing retail kitchens-must match equipment dimensions exactly to available floor area before purchase.
MB Food Equipment provides detailed specifications including height, width, depth, and weight for all available machinery. This technical precision prevents costly delays from equipment that arrives too large for your production area. Additionally, weight ratings matter for floor load capacity, particularly in older Richmond Hill buildings where structural limitations may restrict placement of heavy machinery.
5. Availability of Parts and Technical Support Ensures Operational Continuity
Equipment from discontinued product lines or obscure manufacturers poses a risk: replacement parts become difficult or impossible to source, and technician expertise fades as machines age out of active service. When evaluating used packaging equipment through MB Food Equipment, machinery from established manufacturers with ongoing parts distribution is prioritized. Common brands maintain parts availability for 15 to 20 years, while lesser-known equipment may become orphaned within 5 years.
Richmond Hill businesses also benefit from MB Food Equipment's connection to supplier networks and technician resources throughout the Greater Toronto Area. Equipment sourced through this business comes with guidance on maintenance, part sourcing, and service providers familiar with the machinery you purchase. This support network is invaluable when urgent repairs are needed to keep your operation running.
If you operate a bakery, deli, grocery store, or food manufacturing facility in Richmond Hill and need reliable used packaging equipment, contact MB Food Equipment to discuss your requirements. They can evaluate your space, production volume, and material specifications to match you with equipment that meets your operational needs and budget.
Frequently Asked Questions
What types of packaging equipment does MB Food Equipment supply to Richmond Hill?
MB Food Equipment supplies vacuum sealers, form-fill-seal machines, shrink wrap systems, labeling equipment, and specialized packaging machinery sourced from commercial food operations. Each unit is inspected for operational performance before delivery to Richmond Hill facilities.
How do I know if used packaging equipment will work with my current film and materials?
Specifications including seal width, temperature range, and film thickness compatibility are documented for all equipment. Contact MB Food Equipment with your material type and thickness, and they will confirm compatibility before purchase.
Is there availability of repair parts for used packaging equipment in Richmond Hill?
MB Food Equipment prioritizes equipment from manufacturers with active parts distribution networks. They also maintain connections to technicians and suppliers throughout the Greater Toronto Area who service the machinery they sell.
How much space do commercial packaging machines typically require?
Footprints vary by machine type: horizontal form-fill-seal units typically require 8 feet by 4 feet, while vertical systems may use 5 feet by 3 feet. Exact dimensions are provided for every unit, and MB Food Equipment can advise on placement based on your facility layout.